Build-to-Print Steel for OEMs & Volume Programs
Mona Steel LLC, headquartered in Anaheim, California, makes steel parts and profiles to your drawings in production quantities: roll-formed C, Z, U, hat and sigma sections, laser-cut and bent parts, with the material, processing and coating on one purchase order.
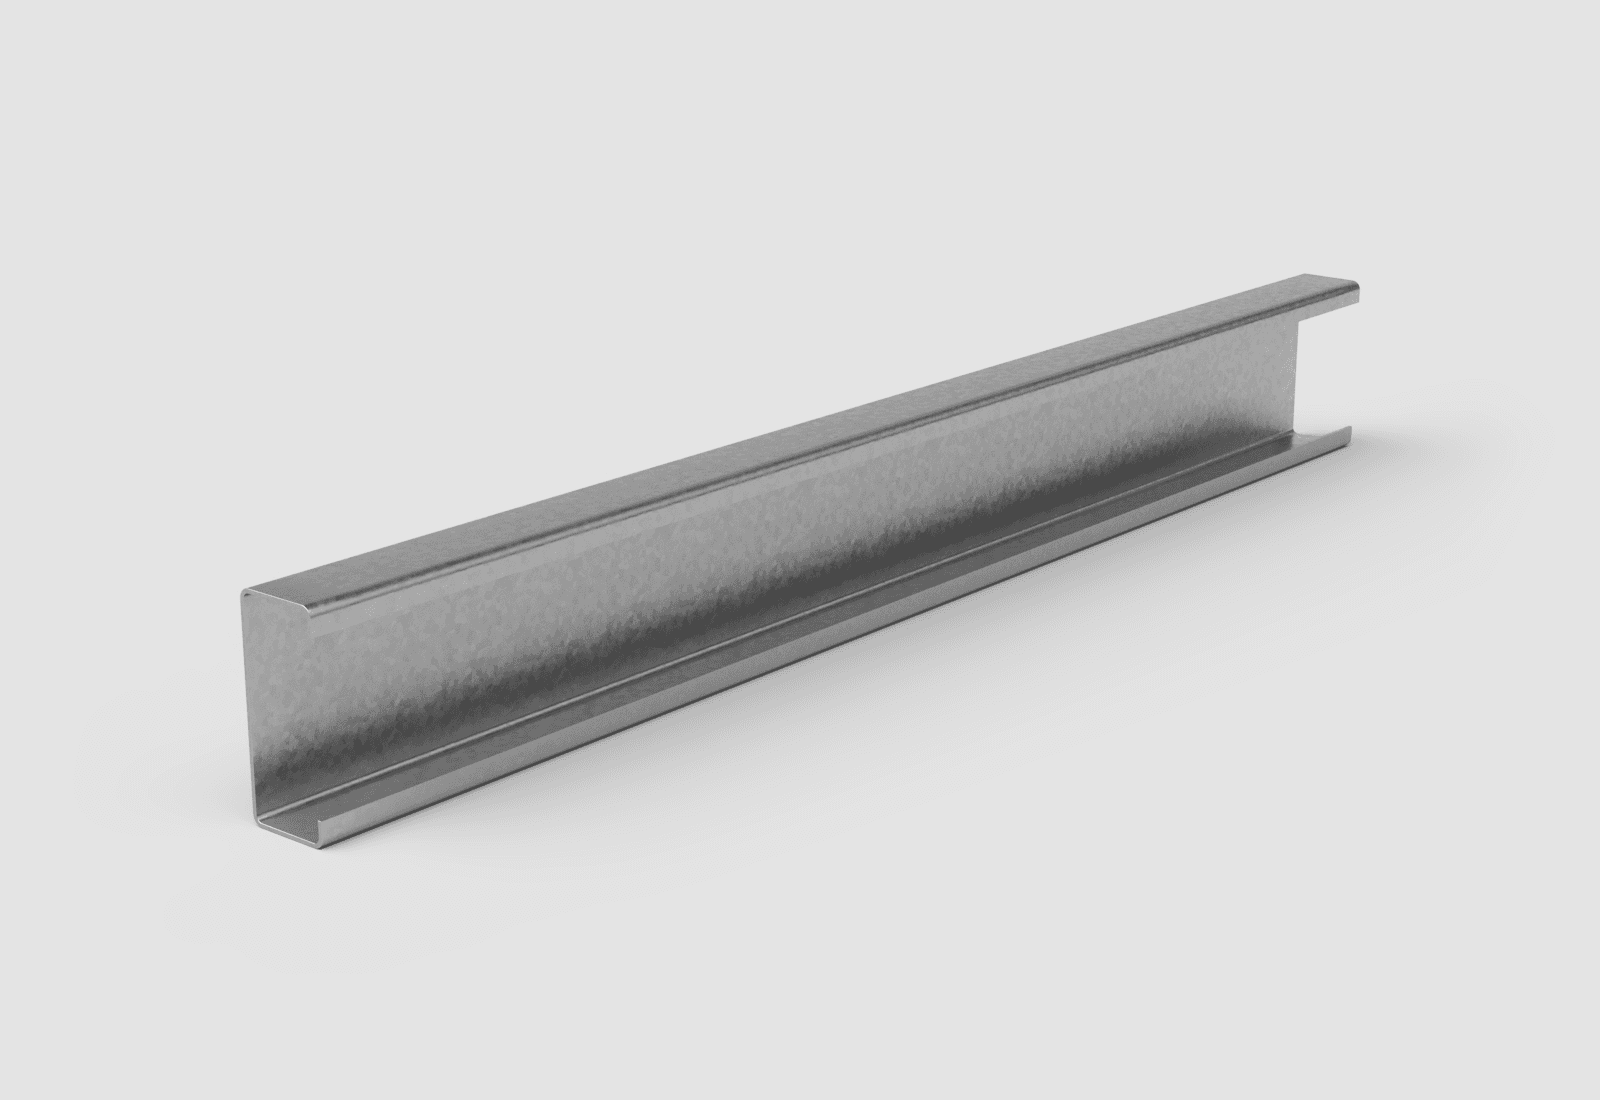
For program buyers, at a glance
- Built to
- Your drawings, revision, grade and coating
- Profiles
- C, Z, U, hat and sigma, 20 ga to ¼ in.
- Parts
- 20 kW laser cutting, press brake bending to 26 ft
- Paperwork
- Mill test reports and heat-number traceability
- Releases
- Repeat releases, labeled by part number
Equipment builders, racking and solar racking companies, metal building suppliers and other manufacturers buy the same steel parts release after release. We make those parts to your print, at your revision, in your grade and coating, in production runs and repeat releases.
Use us for contract manufacturing: as an extension of your shop, as the outside volume supplier for a profile or part you don’t want to run in-house, or as a second source alongside the supplier you already have. Our estimating team reviews every request and comes back with an itemized quote.
Parts and profiles we make to your print
Roll-formed profiles
C-channels, C and Z purlins, U-channels, hat/omega and sigma sections from 20 gauge to ¼ in., with inline pre-punching, slotting, embossing and cut-to-length. New profiles get roll tooling designed for them; an existing one can be matched from a drawing, a sample or a photo.
Production laser-cut parts
Brackets, clips, gussets, splice and connection plates, flanges and panels cut on a 20 kW fiber laser in carbon steel, stainless, aluminum and galvanized sheet, from thin-gauge sheet through heavy plate.
Press-brake formed parts
Channels, angles, brackets, guards and enclosures formed on CNC press brakes, up to 26 ft long and up to 1 in. thick depending on bend length and grade. Cutting and bending in one flow keeps hole locations true after the bend.
Kits on one order
Profiles and the clips, splice plates and brackets that connect them, cut, formed and delivered together on one purchase order, with mill test reports for both.
Rolled shells and heavy plate
Cylinders, cones and segments rolled up to 16 ft in diameter and up to ¾ in. thick, and heavy plate parts cut on CNC plasma and oxy-fuel.
Welding and coating, coordinated
Welding, hot-dip galvanizing (ASTM A123) and powder coating are coordinated in the same order. Profiles can also be formed from pre-galvanized G90 (ASTM A653) or zinc-magnesium coated steel.
Custom roll forming Sigma profiles Production laser cutting Press brake bending
How a build-to-print program runs
A new part or profile goes through all five steps. Once a part is approved, repeat releases run from step four, to the same drawings and files.
- Step 01
Drawings & revision
Send DXF, DWG or STEP files or dimensioned PDFs, each with its revision, plus material, thickness, coating and quantities.
- Step 02
Design review
We check geometry, hole sizes, bends and tabs for manufacturability, suggest cost-saving alternatives and flag problems before production.
- Step 03
Tooling & first articles
For a new profile, roll tooling is designed and first articles are produced for fit-up and testing before production starts.
- Step 04
Production releases
Consistent runs with inline punching and cut-to-length, and laser parts nested across sheets to cut scrap, released to your schedule.
- Step 05
Labeled delivery
Releases are bundled and labeled by part number, phase or sequence and delivered to your shop or job site with mill test reports.
Repeat releases and program pricing
Send the quantity per release and the expected annual usage with your drawings, and the quote covers both the release in hand and the program behind it. On roll-formed profiles, longer runs bring the cost per foot down because setup is spread across more feet of profile. On laser-cut parts, unit pricing improves as quantity increases because setup and nesting are spread across more parts.
Standard parts repeat cleanly from release to release: the same drawings and files produce the same parts. When a drawing changes, send the new revision; revisions are re-released by part, so only the parts that changed are remade.
Roll forming pays off once a profile runs into thousands of linear feet. We also quote smaller orders when we can help: for short quantities the same section can often be brake-formed, and we price both so you can see the break-even point.
Documentation, packaging and labels
- Mill test reports
- Material comes with mill test reports (MTRs) and heat-number traceability on every order, for your QA/QC records.
- Coating certificates
- Galvanizing certificates where coatings apply.
- Other documents
- Anything else your quality team or your customer requires, listed in the request so it is quoted up front rather than requested at delivery.
- Labels
- Releases are bundled and labeled by part number, phase or install sequence. Tell us the label each bundle needs and it is covered in the quote.
- Bundles
- Bundle size and weight limits set to what your crew can unload.
- Staging
- Releases staged to your schedule and delivered to your shop or job site.
A second source for roll-formed and laser-cut parts
Many manufacturers keep a second source for the profiles and parts their products depend on, or hand repeat volume to an outside supplier so their own lines stay free for other work. We can make a part alongside your current supplier, take on a profile you no longer want to run in-house, or quote overflow releases when demand runs ahead of your own lines.
Qualifying a second source starts with the drawing and revision, the grade and coating, and a sample if you have one. An existing profile can be matched from a drawing, a sample or a photo with key dimensions, and first articles are produced for fit-up and testing before production releases start, so parts from both sources are made to the same drawing, revision, grade and coating.
Mona Steel LLC is headquartered in Anaheim, California. Deliveries go to plants and job sites across Southern California, the Central Valley and the rest of the state, and to Texas, Arizona, Nevada and nationwide, quoted per load and staged to your release schedule.
Industries we make parts for
Typical build-to-print programs:
- Machinery and equipment: laser-cut blanks and parts, formed panels and guards, frames and rolled shells
- Warehouse and storage racking: pallet racking uprights, beams and custom profiles
- Solar racking: rails, purlins, hat and sigma sections, brackets and splice plates
- Metal buildings: C and Z purlins and girts
- Agricultural equipment: C, Z and U members up to ¼ in. thick, and laser-cut parts
- Data center framing: C and Z purlins and girts, and pre-punched support channel for trapeze supports
- Greenhouse structures: roll-formed profiles and tube
- Truck, trailer and conveyor parts: long-length formed members and heavy brackets
Data center steel Solar racking and tracker parts C and Z purlins All industries
What to send for a program quote
Send what you have; our estimating team reviews every request and comes back with an itemized quote. The more of this list it covers, the firmer the price.
| Item | What to send | Why it matters |
|---|---|---|
| Drawings and revision | DXF, DWG or STEP files, or dimensioned PDFs, each with its revision; for an existing profile, a sample or a photo with key dimensions | Parts are quoted and made to that revision |
| Material grade and thickness | ASTM specification and grade, and the decimal thickness, with the gauge as a reference only | One gauge number maps to different decimals on different charts |
| Coating | Pre-galvanized (e.g., G90), hot-dip galvanized after fabrication, zinc-magnesium, powder coat or bare | The finish sets the material ordered and how cut edges are prepared |
| Quantity per release | Pieces per part number, or linear feet per profile | It sets the run length, which drives setup cost per part and per foot |
| Annual usage | Expected annual usage of each part or profile | The quote can cover the program, not just the first release |
| Release cadence | How often releases are needed, such as monthly or by phase | Production and deliveries are scheduled to it |
| Packaging and labels | Bundle size and weight limits, and the label each bundle needs | Packaging is covered in the quote instead of added at delivery |
| Delivery ZIP codes | Every delivery ZIP code, with any staging by plant, phase or job | Deliveries are quoted per load |
| Documents | Mill test reports, galvanizing certificates and anything else your customer requires | Documents are quoted up front rather than requested at delivery |
For a profile, add the hole and slot pattern as a DXF or drawing, and each length with its piece count.
Roll-formed profile RFQ checklist Laser cutting cost guide Request a quote
Build-to-print steel FAQ
What does build to print mean for steel parts?
Build to print is a form of contract manufacturing: the supplier makes the part to the customer’s own drawing, revision and specifications instead of designing it. Mona Steel LLC makes roll-formed C, Z, U, hat and sigma profiles and laser-cut and press-brake-formed parts to your print, in the grade and coating you specify, in production runs and repeat releases.
Can you be a second source for a roll-formed profile we already buy?
Yes. Send the drawing and revision, the grade and coating, and a sample if you have one; an existing profile can also be matched from a photo with key dimensions. If the profile needs new roll tooling, it is designed first, and first articles are produced for fit-up and testing before production releases start.
Can a build-to-print program start with prototype quantities?
Yes. Equipment builders use Mona Steel LLC from prototype quantities to repeat production releases. For a new roll-formed profile, tooling is designed and first articles are produced for fit-up and testing; for short quantities, the same section can often be brake-formed instead, and we price both so you can see the break-even point.
How is a repeat steel parts program priced?
Send the quantity per release and the expected annual usage with your files, and the quote covers both the release in hand and the program behind it. Longer roll-forming runs bring the cost per foot down because setup is spread across more feet of profile, and on laser-cut parts unit pricing improves as quantity increases because setup and nesting are spread across more parts. Every quote is itemized by part.
Can roll-formed profiles and laser-cut parts go on one purchase order?
Yes. Profiles and the laser-cut and press-brake-formed clips, splice plates, connection plates and brackets that go with them are quoted and delivered together on one purchase order, with mill test reports for both. Welding, hot-dip galvanizing and powder coating are coordinated in the same order.
Can you label bundles with our part numbers?
Yes. Releases are bundled and labeled by part number, phase or install sequence and staged to your schedule. Put bundle size and weight limits and the label each bundle needs in your request, so they are covered in the quote.
What happens when a drawing revision changes?
Send the new drawing or file with its revision. Revisions are re-released by part, so only the parts that changed are remade. If the change alters a roll-formed section, say so early, because roll tooling is designed for the profile.
Who is responsible for the design of a build-to-print part?
You are, or your engineer of record. Build to print means we make the part to your drawing and specifications; Mona Steel LLC doesn’t provide stamped structural engineering or sealed connection design. Any change suggested in our design review goes back to you for approval before it is made.
Request a quote
Send the drawings for your next program.
Drawings or files with their revision, the grade and coating, the quantity per release and the annual usage. Our estimating team reviews every request and comes back with an itemized quote.
- DXF
- DWG
- STEP
- XLS/CSV